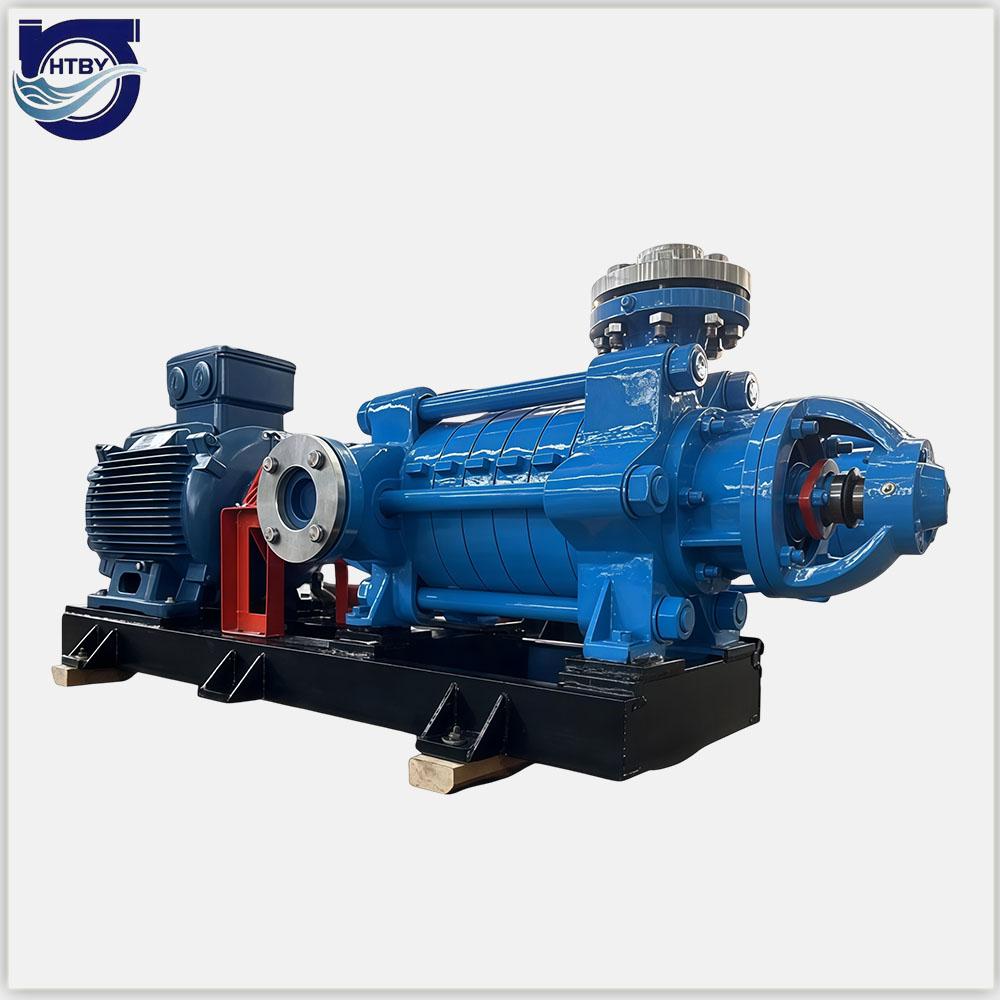
D DG Multistage Pump
D & DG are horizontal segmental single-suction multistage centrifugal pumps for clean water (impurity ≤1%, particle ≤0.1mm) and analogous liquids. Max medium temp: D ≤80℃, standard DG ≤105℃, customized DG ≤120℃. Standard D has horizontal suction & vertical upward discharge; oilfield-type D and all DG feature vertical upward inlet & outlet. Fitted with packing seal: D uses internal pump fluid for seal water while DG adopts external water supply, driven by motor via elastic coupling.
Product details
Product Features
1.Compact segmental construction for easy disassembly and maintenance;
2.Fully sealed anti-rust shaft avoids medium corrosion;
3.Optional packing/mechanical seal, stable performance & easy servicing;
4.Optimized hydraulic design: high efficiency, wide performance range, low noise;
5.Custom material available for corrosive oilfield water injection.
Main Application
· D type (≤80℃): mine drainage, industrial & municipal water supply, oilfield water injection;
· DG type (std≤105℃ / custom≤120℃): medium & small boiler feedwater, clean hot water transfer.
Model Designation
For example:
Model: D (DG)155-67*9
D-Multistage centrifugal water pump
DG-Multistage boiler feed pump
155-Flow (m³/h)
67-Single-stage head (m)
9-Number of stages
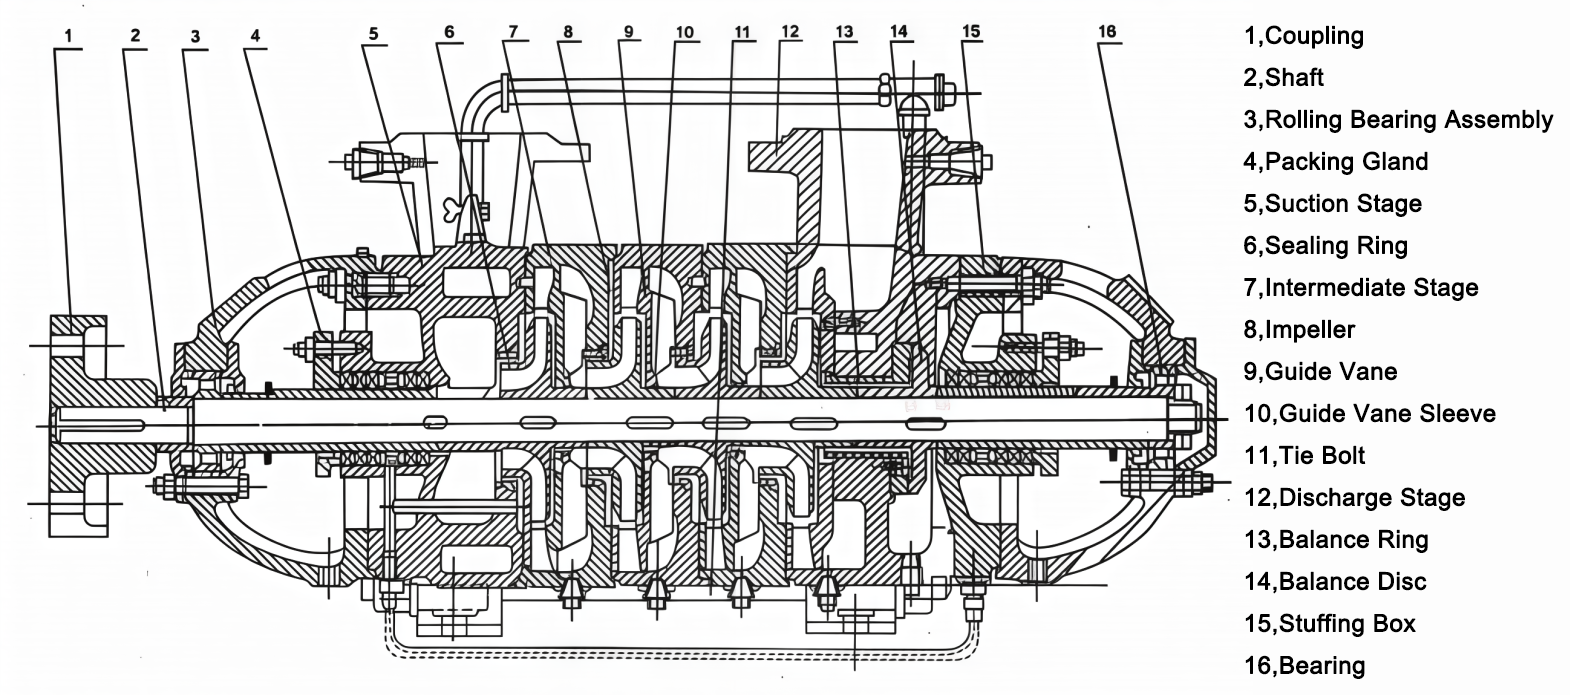
D Multistage Pump Structure Diagram
More products
Explore Related Pump Models

HTAH, HTM, HTHH Slurry Pump
HTAH, HTM and HTHH horizontal centrifugal slurry pumps for abrasive, high-concentration slurry in mining, metallurgy, coal and power applications. Compare HTAH models and performance data below. Send your flow, total head and slurry details to discuss pump selection and request a quotation.
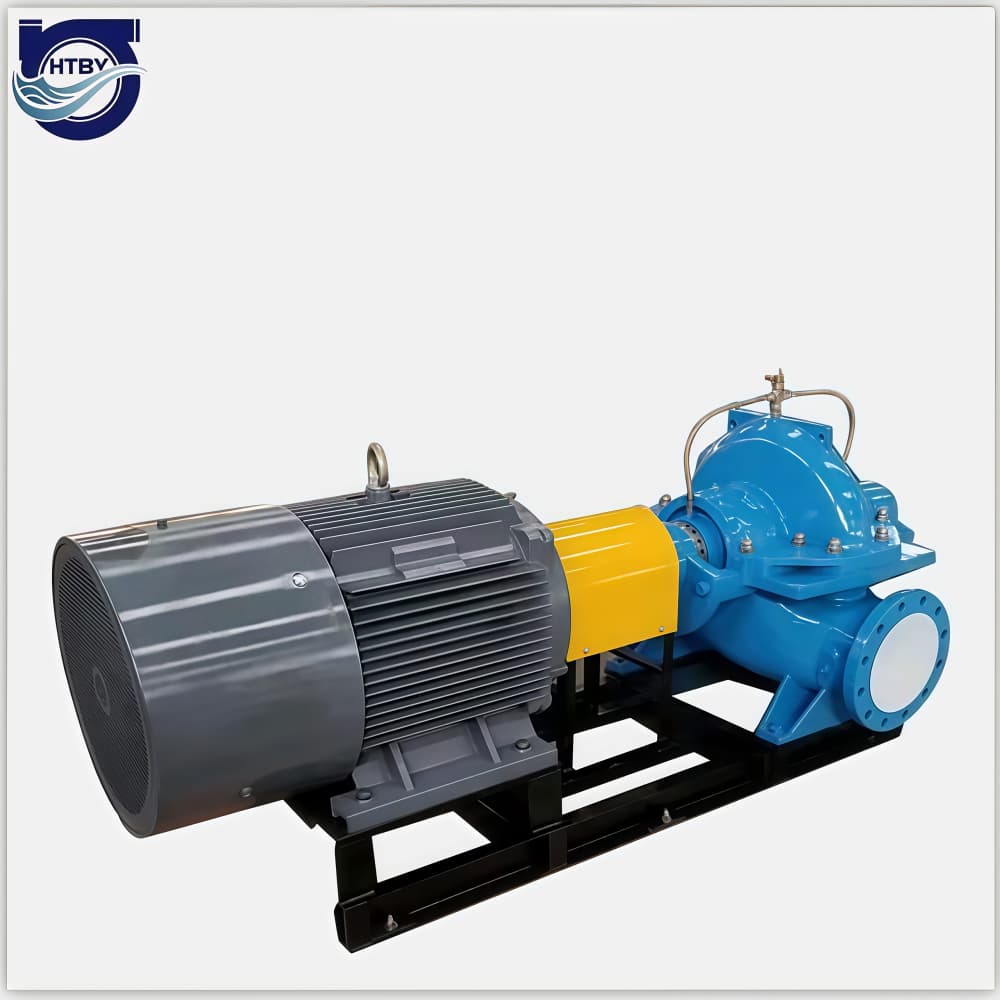
S SH Split Case Pump
S/SH is horizontal single-stage double-suction split case centrifugal pump for clean water or medium with water-like properties; permissible medium temperature ≤80℃. Split casing enables overhaul without detaching inlet/outlet piping or motor; standard rotation is counterclockwise viewed from coupling side.
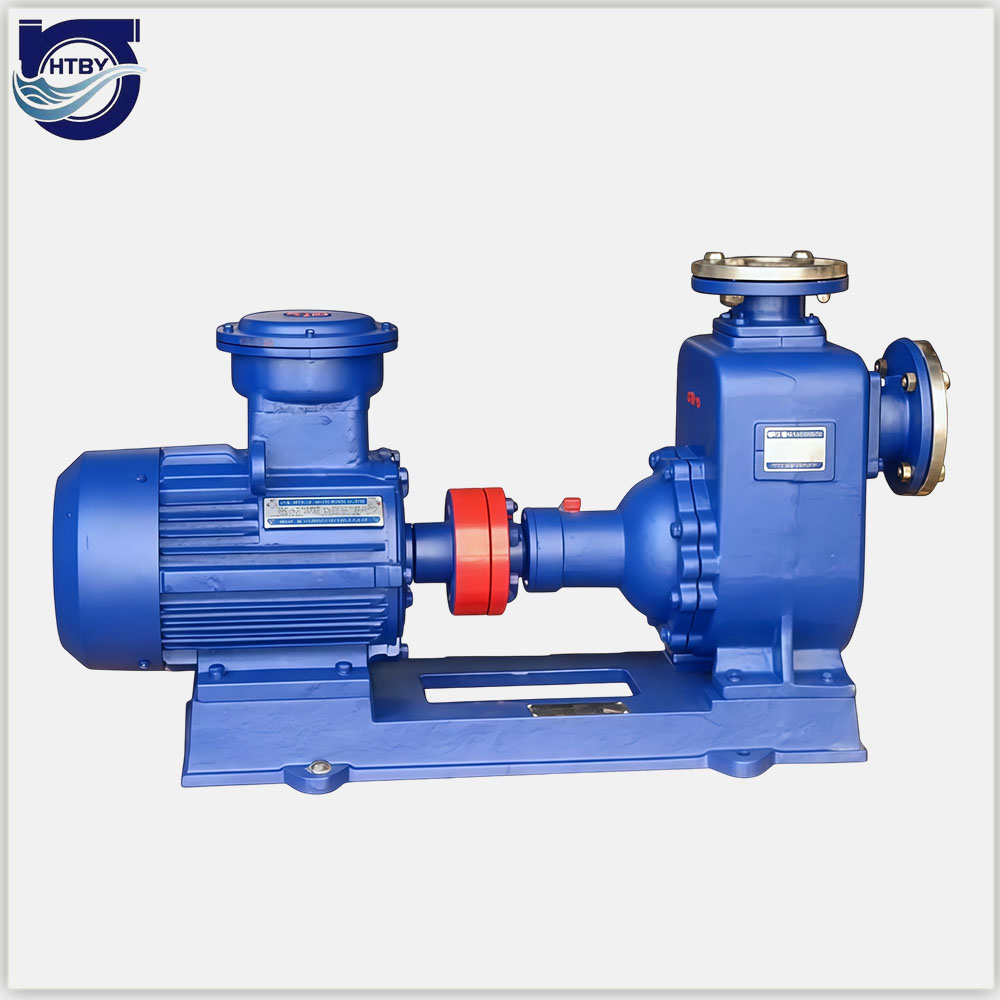
ZX Self-Priming Pump
The ZX self-priming sewage pump is characterized by stable performance, high operational reliability, high efficiency, low noise, compact structure, aesthetic appearance, and ease of installation and maintenance. As a new-generation energy-efficient product, it represents the most ideal option among current self-priming oil transfer pumps. The series is widely applicable in industries such as petroleum, chemical, pharmaceutical, environmental protection, urban construction, mining, transportation, and electric power.
Need a pump solution for your application?
Share your operating conditions and requirements with our team. We’ll help identify a suitable pump configuration.
Get a quote